New MaxiLobe Pumps Target Higher Efficiency and Lower Lifecycle Costs
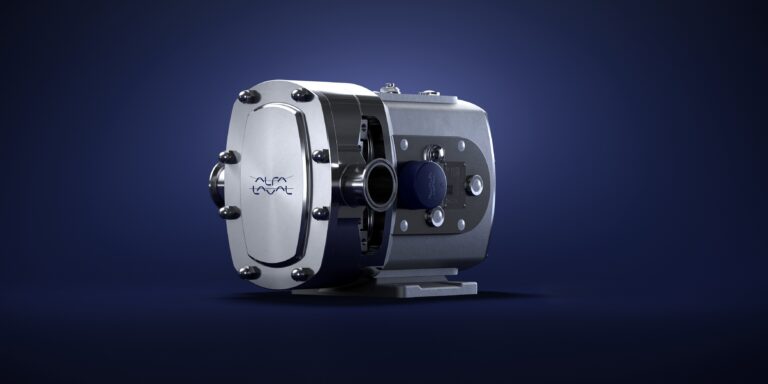
Rotary lobe pump from the new Alfa Laval MaxiLobe range (Image source: ALFA LAVAL Corporate AB)
Use in Hygienic Processes
Manufacturers in the dairy, food, beverage, home and personal care, and pharmaceutical industries are under constant pressure to improve efficiency, maximize uptime and reduce the total cost of ownership. Alfa Laval has designed the MaxiLobe and MaxiLobe UltraPure pump ranges for these applications, with higher volumetric efficiency, a broader operating envelope and simpler service.
“For decades, our rotary lobe pumps have been widely used in hygienic and high-purity processing where reliability and predictable performance are essential,” says Russ Kelly, Portfolio Manager, Pumps at Alfa Laval. “MaxiLobe builds on that legacy with improved hygienic design across a wider operating range, enabling smaller pumps to achieve the same duty at lower speeds. Lower speeds reduce shear, helping improve operating efficiency and safeguard shear-sensitive products.”
Optimized Investment
MaxiLobe and MaxiLobe UltraPure pumps are designed to help optimize capital investment through high volumetric efficiency and a broad flow and pressure envelope. Additionally, by enabling a smaller pump to be selected for the required duty in suitable applications, MaxiLobe can reduce equipment and installation costs, including the associated electrical equipment. This reduces the need for oversizing while maintaining operational flexibility.
Key porting dimensions match those of all Alfa Laval SRU pumps and most SX and SX UltraPure models, allowing replacement without modifying existing pipework. Under defined operating conditions, MaxiLobe delivers at least 5% higher flow rates than the equivalent SRU model, improving process capacity without increasing footprint or installation complexity.
Cost-Effective Operation
MaxiLobe and MaxiLobe UltraPure pumps can deliver the required flow rates at lower operating speeds, helping reduce energy consumption and electricity costs. Operating the pumps at lower speeds also reduces shear on sensitive products that may be damaged when operating at higher speeds. By reducing mechanical stress, MaxiLobe pumps can help extend service intervals and equipment life.
A robust gearbox design is intended to support reliable performance under demanding conditions, reducing the risk of unplanned stoppages and supporting more predictable, resource-efficient operation and lower lifecycle costs.
Hygienic Design
Precision-profiled elastomers, good cleanability and a hygienic and high-purity design are intended to protect product quality and reduce cross-contamination risk. MaxiLobe provides both EHEDG and 3-A certification alongside full FDA compliance as standard.
For pharmaceutical and biotech applications, MaxiLobe UltraPure complies with ASME BPE standards and Good Manufacturing Practices guidelines. It offers material options, enhanced surface finishes and product-wetted materials conforming to FDA and USP requirements. Alfa Laval Q-doc documentation provides traceability and validation support for use in regulated manufacturing environments.
Every pump is factory-tested and supplied with a performance certificate confirming that it meets its specified operating curve before delivery.
Simpler Service
MaxiLobe and MaxiLobe UltraPure are engineered for quick, predictable maintenance. Front-loading single seals can be replaced without removing the pump from the process line, reducing downtime during routine service. Interchangeable components and easily accessible shimming are designed to simplify servicing and help reduce maintenance time.
Source: ALFA LAVAL Corporate AB