Edwards Celebrates Its 500,000th Rotary Vane Pump – A Milestone in Rotary Vane Technology
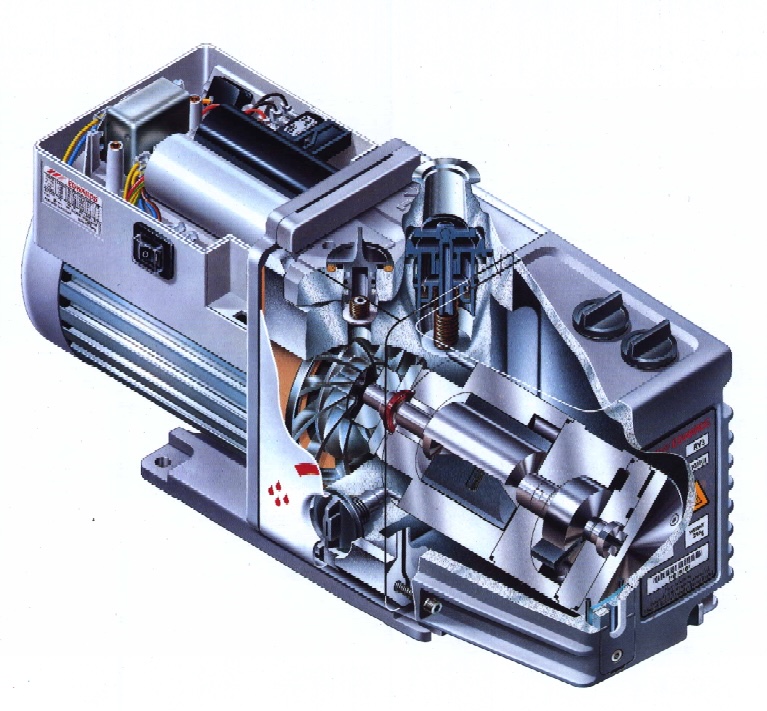
Launched in 1994, the pump was the first Edwards product to carry the ‘CE’ badge, signifying compliance with European standards. (Image source: Edwards Ltd.)
This achievement is the result of both ambitious thinking and the engineering excellence to bring it to life.
Breaking new ground – a pioneer’s journey
Single-stage rotary vane pumps like the EM and E2M once dominated Edwards' RV range. Yet the journey to innovation began when engineers saw more than just a gap in the market—they saw the potential to redefine what was possible.
“We saw this as an opportunity to make something new. Easy to manufacture, easy to maintain, and with longevity at its heart,” says David Goodwin, who has guided the RV project since the early 1990s and is now retired after four decades as Product Manager.
“The market for RV pumps had expanded to include laboratories and light-industrial users, alongside to traditional OEM and R&D customers. This shift created a demand for pumps that not only delivered better performance, but were quieter, reliable, easy to maintain, and wouldn’t look out of place on a lab workbench.”
From concept – to drawing board – to prototype
Alan Holbrook was the Senior Development Engineer and led the team responsible for turning this vision into reality.
“One of the key challenges was making two pumps function as one. No one else had a two-stage RV pump capable of handling water vapor, and it was overcoming these obstacles led to one of the product’s key patents.”
Planning had begun in the late 1980s, but by 1990, Alan and his team were in full swing, deconstructing the design to its core principals and reimagining and well as reengineering it from the ground up.
“We initially set out to design a pump that could be built using a fully automated robotic system. While we achieved that, we also created a pump that was so much simpler to assemble that even manual production times were comparable to automation.”
The RV pump also introduced important features such as:
- A mode-switch feature allowed users to seamlessly transition between high-vacuum and high-throughput operation
- Fast acting inlet for system protection
- A robust design built to withstand a variety of environments.
Launched in 1994, the pump was the first Edwards product to carry the ‘CE’ badge, signifying compliance with European standards.
Reliable, consistent workhorse
While economic and industrial cycles have fluctuated over the past 40 years, the RV pump has sustained relatively steady year-on-year production levels and remains as relevant and viable today as it did when it first launched.
Renowned as a dependable workhorse, its lasting success speaks to the value it brings to customers, as demonstrated by it winning the ‘BOC Technology Award’ in 1993.
“The rotary vane pumping mechanism itself has been perfected close to the limit, making the RV pump a highly praised, universal, robust and reliable product.” notes Boris Marecak, the current Product Manager.
As the RV pump enters its next chapter, the industry faces a significant evolution: the transition from oil-sealed systems to dry alternatives. This “wet-to-dry” strategy represents one of the biggest challenges for oil-sealed pumps, as sustainability and carbon footprint reduction become central to product development.
“There is no single focus area going forward,” Boris explains. “Sustainability and carbon footprint reduction are the forefront. We aim to optimise the product, localise production to reduce transportation costs, and develop new ways to lower power consumption, operational expenses, and total cost of ownership.”
This evolution is not about radical change, but about steady, thoughtful progress. The RV pump will continue to serve many of Edwards’ most valued customers, remaining a key solution in their operations. The future includes expanding and simplifying motor offerings and implementing smart features that deliver real value to users.
Oil-sealed pumps continue to hold a strong position in the market and remain essential for many customers. The outlook for this technology is promising, not through sudden revolution, but through steady evolution and a commitment to continuous improvement.
Celebrating the past, engineering the future
With over 500,000 units produced, the RV pump stands as a testament to Edwards’ legacy of innovation and reliability. As we look ahead, the RV continues to evolve—driven by sustainability, smart technology, and a deep understanding of our customers’ needs. The journey is not over; it is entering a new chapter, and the best may be yet to come.
Source: Edwards Limited