Atlas Copco Introduces the New GHS 402 – 902 VSD⁺ Screw Pump
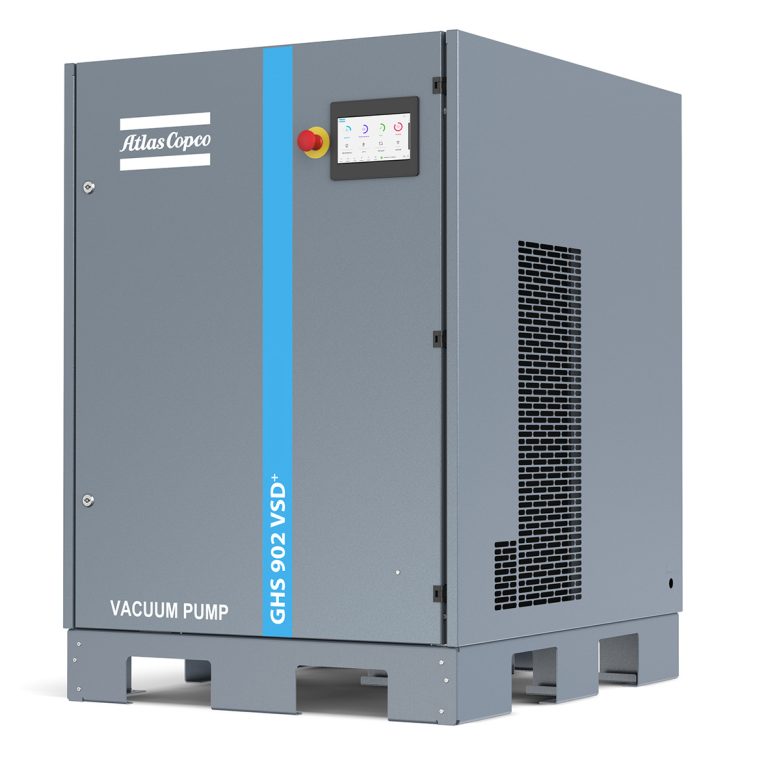
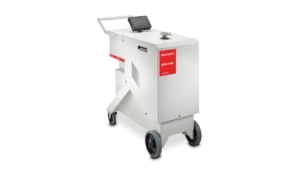
With the introduction of the GHS VSD⁺ vacuum pump series, Atlas Copco has taken vacuum technology to a new level. (Image source: Atlas Copco AB)
In keeping with this tradition, Atlas Copco has developed the new GHS 402 - 902 VSD⁺ vacuum pump, in which the process vacuum depends on the flow requirement and is controlled by constant pressure setpoint control in the vacuum. This 2nd generation of the pump brings innovation delivering high pumping speeds - from atmospheric pressure to ultimate pressure. For users, this results not only in energy savings but also to faster pump down performance. With these attributes, the GHS 402-902 VSD+ is particularly suitable for food packing, vacuum cooling of flowers and vegetables and thermoforming of plastics and white goods.
Engineered for performance, designed for sustainability
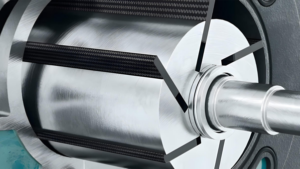
The GHS 402 - 902 VSD⁺ models set the benchmark in vacuum performance. Equipped with our next-generation oil-injected screw element, a highly efficient IE5 motor, and advanced HEX@™ connectivity, these pumps deliver intelligent performance, longer maintenance intervals, lower operating costs, and an overall lower environmental impact. “With higher pumping speeds and class leading efficiency across the entire pressure range, the GHS 402–902 VSD⁺ dramatically cuts power usage—directly improving our customers’ bottom line while supporting their sustainability goals” reports Product Manager Ilias Alafogiannis.
With a new vertically mounted, fully integrated oil-cooled drivetrain, the GHS 402–902 VSD⁺ series deliver clear ergonomic and operational advantages—including lower noise levels and a compact footprint of less than 1 m². The optimized oil-separator vessel further enhances oil retention, ensuring a cleaner exhaust and reduced environmental impact.
“With a design 30% more compact and oil-discharge levels cut by half compared to previous models, combined with noise-dampening canopy, these pumps are ideal for both central vacuum systems and point of use applications – bringing significant improvements to the working environment of any production facility,” explains Ilias Alafogiannis.
The most important advantages of the GHS 402 – 902 VSD⁺ at a glance:
- Modern, oil-injected screw element with compression optimization valves offering high performance from atmospheric pressure and lower power consumption
- Compact design with footprint of less than 1 m²
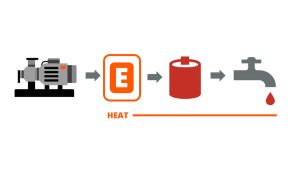
- Recovery of up to 80 percent of pump heat as reusable hot water
- HEX@ intelligent controller enabling Industry 4.0 features as remote monitoring, intelligent control, and diagnostics
- Lower noise levels, better oil retention and longer maintenance intervals.
Source: Atlas Copco AB