Amarinth Delivers Interchangeable Cryogenic Pump Replacements for Air Products
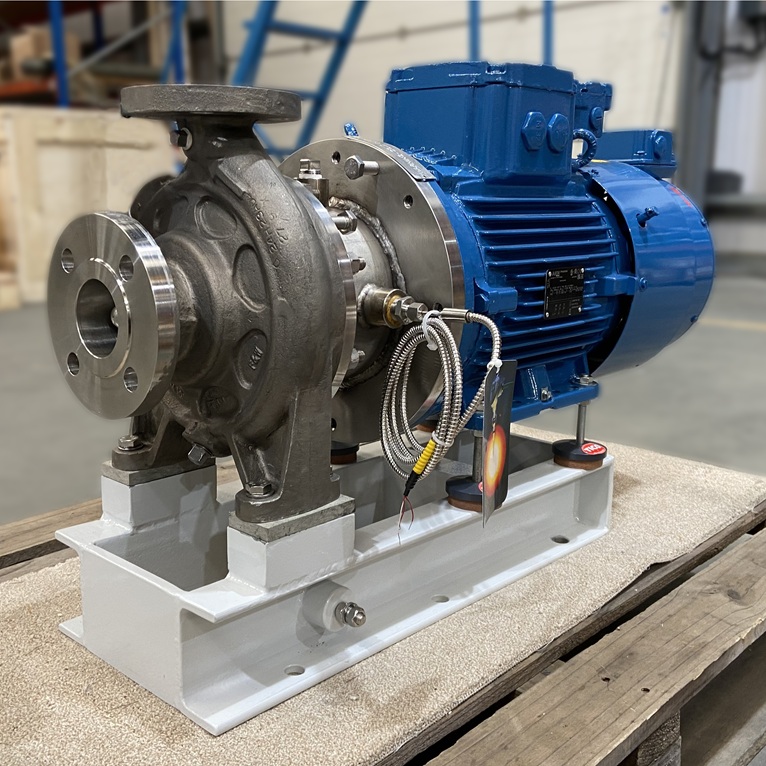
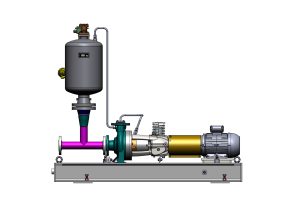
Amarinth Cryogenic Pump (Image source: Amarinth Ltd.)
Over 30 years ago, Girdlestone Pumps supplied Air Products with cryogenic 950 series pumps designed for low Net Positive Suction Head (NPSH) operations. While these assets provided decades of reliable service, they eventually required full replacement. However, because Girdlestone and its original product lines are now obsolete, sourcing direct replacements presented a significant procurement challenge.
Air Products turned to Amarinth, which has a proven industry-wide reputation for providing dimensionally and hydraulically interchangeable solutions for obsolete Girdlestone pumps. Furthermore, Amarinth had successfully supplied Girdlestone 950 replacements to Air Products on a previous project. The plug-and-play capability of Amarinth’s pumps eliminates the need for costly, time-consuming modifications to existing facility pipework and fittings. Combined with its extensive technical expertise in low NPSH and specialised cryogenic applications, Amarinth was uniquely positioned to deliver an advanced, modern replacement.
Beyond providing a seamless physical interchange, Amarinth addressed a material compliance requirement for the fluid barrier. The original pump supplied by Girdlestone utilised a carbon loaded PTFE bushing to segregate the liquid nitrogen from the gas contained in the lantern / motor assembly. Air Products advised that the replacement pump should be FDA (Food and Drug Administration) compliant. The metallurgy was fine, however to meet FDA compliance carbon loaded PTFE was not allowed in contact with the liquid nitrogen. Amarinth therefore sourced a new material that would perform the sealing duties and was suitable for both FDA compliance and the cryogenic application.
Amarinth also redesigned the mounting feet for the motor and pump assembly, replacing the old rubber mounted feet in the Girdlestone pump. The upgraded mounting feet use an advanced new material to safely and reliably absorb the dimensional changes caused by the cryogenic temperatures of the pumped fluid, maintaining precise alignment between the motor and pump.
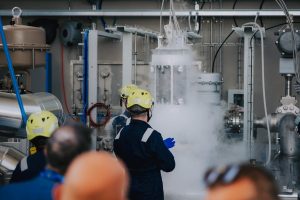
The new pumps are manufactured from high-grade stainless steel to cope with cryogenic temperatures, maintaining structural integrity and long-term durability against thermal stresses. To meet strict quality control standards, comprehensive Non-Destructive Testing (NDT) was carried out across the pump components. Furthermore, to validate the integrity of the design before deployment, the pumps underwent rigorous cold start testing using liquid nitrogen to replicate real-world process conditions.
Oliver Brigginshaw, Managing Director of Amarinth, commented: “We are delighted to have delivered this technically sophisticated replacement project for Air Products. It perfectly highlights our unique ability to combine our deep knowledge of legacy Girdlestone assets with modern engineering innovation. By introducing cutting-edge materials to solve age-old issues like thermal shrinkage and vibration in cryogenic pumps, we provide our customers with robust, future-ready pumping solutions that minimise lifecycle costs and eliminate the need for disruptive infrastructure changes.”
Source: Amarinth Ltd.